Industry Knowledge
Why Proof Load Matters More Than Tensile Strength When Specifying Carbon Steel Bolts
Most buyers focus on the tensile strength grade when ordering Carbon Steel Bolts — 8.8, 10.9, or 12.9 — but the specification that determines whether a bolted joint remains clamped under service conditions is proof load, not tensile strength. Proof load is the maximum axial force a bolt can sustain without taking any permanent set. Once tightened beyond the proof load, the bolt stretches plastically and clamp force drops unpredictably, leading to joint relaxation, fretting, and eventual fatigue failure even when the bolt itself hasn't fractured.
Proof Load vs. Tensile Strength by ISO 898-1 Grade
| Grade |
Min. Tensile Strength |
Proof Load Stress |
Proof Load / UTS Ratio |
Typical Application |
| 4.8 |
420 MPa |
310 MPa |
~74% |
Light static loads, general machinery |
| 8.8 |
800 MPa |
600 MPa |
~75% |
Steel structures, automotive chassis |
| 10.9 |
1040 MPa |
830 MPa |
~80% |
Engine components, suspension joints |
| 12.9 |
1220 MPa |
970 MPa |
~79% |
High-load precision assemblies |
In automotive fastener applications — an area where Shanghai Soverchannel Industrial Co., Ltd. has accumulated years of deep technical experience — tightening strategy is specified as a percentage of proof load, typically 70–80%. Torque-angle tightening methods go further by deliberately stretching the bolt into the plastic region in a controlled and repeatable way, maximizing clamp force consistency across a production line without individual bolt variation causing joint-to-joint scatter. The proof load value printed on material test certificates is therefore a mandatory verification point, not an optional data field, for any structural carbon steel bolt procurement.
Hydrogen Embrittlement Risk in High-Grade Carbon Steel Bolts and How to Control It
Hydrogen embrittlement (HE) is a failure mode specific to high-strength carbon steel fasteners — particularly grades 10.9 and 12.9 — that can cause sudden, brittle fracture at stress levels well below the bolt's rated tensile strength. Unlike fatigue or overload failure, hydrogen embrittlement produces no visible deformation beforehand. The bolt fractures without warning, typically within hours to days after tightening, making it one of the most hazardous failure modes in safety-critical assemblies.
The hydrogen source is almost always the electroplating process. Acid pickling before zinc electroplating releases atomic hydrogen that diffuses into the steel lattice. Under tensile stress, this hydrogen migrates to stress concentration points — thread roots, under-head fillets — and reduces the energy needed to propagate a crack. The higher the tensile strength, the more susceptible the steel, which is why HE is predominantly a grade 10.9 and 12.9 concern rather than a grade 8.8 issue.
Process Controls That Reduce Hydrogen Embrittlement Risk
- Baking after plating: ASTM F1941 and ISO 4042 require baking at 190–220°C for 8–24 hours within 4 hours of electroplating for fasteners above 1000 MPa tensile strength. This drives diffusible hydrogen out of the lattice before residual stress in the assembly can trigger crack initiation.
- Alternative coating systems: Mechanical zinc plating (peen plating) avoids the acid pickling step entirely, eliminating the primary hydrogen source. Dacromet and Geomet coating systems similarly apply no hydrogen during processing, making them preferred for grade 12.9 bolts in engine and drivetrain applications.
- Sustained load testing: ASTM F606 Method 4 subjects a sample of plated bolts to 75% of proof load for 48 hours and inspects for fracture. Requesting this test as a lot acceptance criterion for safety-critical grade 10.9 and 12.9 batches provides objective HE-resistance evidence from the actual production lot.
- Minimizing pickling time: Where electroplating is required, limiting acid exposure time and using inhibited pickling acids reduces hydrogen uptake at the source, complementing the downstream baking step.
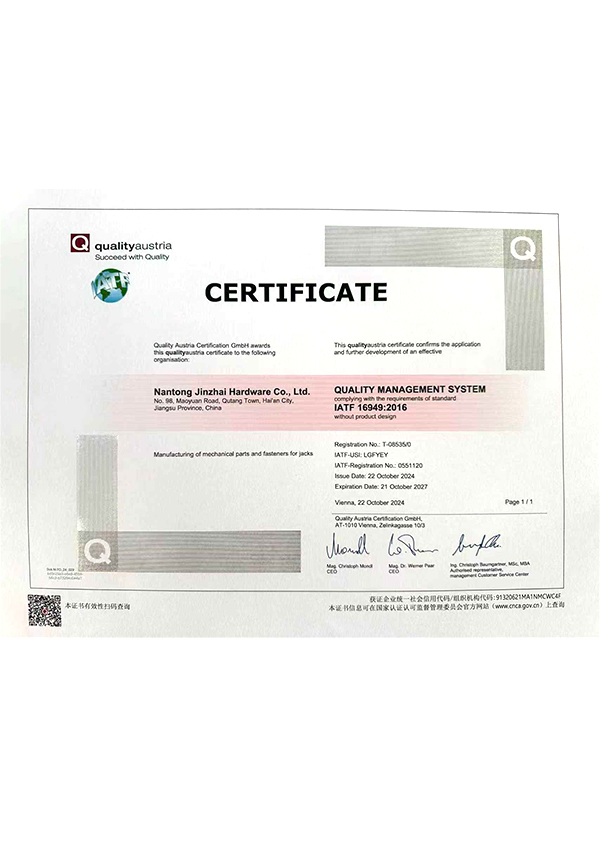
Shanghai Soverchannel Industrial Co., Ltd. applies documented baking protocols and surface treatment traceability through its Nantong Jinzhai Hardware Co., Ltd. manufacturing plant, with process records available to customers requiring HE compliance evidence for automotive and industrial supply chain audits.
Drive Recess Selection for Carbon Steel Screws: Torque Transmission and Cam-Out Resistance
Carbon Steel Screws are available with a wider range of drive recesses than most buyers actively specify — yet the drive selection has direct consequences for assembly line efficiency, joint integrity, and tool life. Cam-out, the phenomenon where the driver tip rides out of the recess under torque, is not just an operator nuisance: it damages the recess, accelerates driver wear, and reduces the installed torque below target by allowing slippage before the specified value is reached. Matching drive geometry to assembly torque and tool type eliminates most cam-out problems at the design stage.
| Drive Type |
Standard |
Cam-Out Resistance |
Torque Transmission |
Best Use Case |
| Phillips (PH) |
ISO 8764 |
Low (designed to cam out) |
Moderate |
Consumer electronics, light assembly |
| Pozidriv (PZ) |
ISO 8764 |
Medium |
Medium-High |
Furniture, general construction |
| Torx / Hexalobular (TX) |
ISO 10664 |
Very High |
High |
Automotive, power tools, appliances |
| Internal Hex (Allen) |
ISO 4762 |
High |
Very High |
Machinery, structural fastening |
| Square (Robertson) |
ASME B18.6.3 |
High |
High |
Wood construction, North America |
The Phillips recess was deliberately engineered to cam out at a predictable torque — an intended feature in 1930s manufacturing where it prevented overtightening of sheet metal screws without torque-controlled drivers. In modern automated assembly with servo-controlled tools, this behavior becomes a liability rather than a feature, and Torx or Pozidriv drives are consistently preferred in high-volume automotive and appliance manufacturing. Shanghai Soverchannel Industrial Co., Ltd. produces carbon steel screws across all major recess types with recess depth and form verified against gauge criteria, ensuring consistent driver engagement across production batches.
Galling Prevention in Stainless Steel Bolts and Screws During Assembly
Galling — the cold welding and tearing of thread surfaces during assembly — is the most common and frustrating failure mode specific to Stainless Steel Bolts and Stainless Steel Screws. Unlike carbon steel fasteners where surface hardness and coatings provide lubrication and wear resistance, austenitic stainless steel (A2, A4) is inherently prone to adhesive wear when identical materials rub under pressure. The oxide layer that provides corrosion resistance is thin and easily displaced by the contact pressures generated during thread engagement, causing the base metal of bolt and nut to cold-weld locally and then tear as rotation continues.
The result is a seized assembly — often permanently — that requires destructive removal and replacement of both the bolt and the mating thread. In petrochemical plants, offshore structures, or food processing equipment where stainless is specified for its corrosion resistance, galling-seized fasteners are a significant maintenance cost and a source of unplanned downtime.
Practical Methods to Reduce Galling Risk
- Dissimilar material pairing: Using A4 (316) stainless bolts with A2 (304) nuts, or pairing austenitic bolts with silicon bronze or brass nuts, breaks the identical-material contact condition that promotes cold welding. Even a small hardness differential between mating threads significantly reduces galling propensity.
- Anti-galling lubricants: Never-Seez (copper-based), Molykote paste (molybdenum disulfide), or PTFE-based thread compounds reduce the coefficient of friction between stainless threads from approximately 0.15–0.20 to below 0.10, preventing the contact pressure spikes that initiate cold welding. Critical note: applying lubricant changes the torque-to-preload relationship by 25–40%, so tightening torque must be recalculated if switching from dry to lubricated assembly.
- Slow assembly speed: Heat generated by friction during rapid assembly accelerates galling initiation. For stainless fasteners larger than M12, manual wrench tightening is consistently less prone to galling than power tool assembly, especially for the first several thread turns where initial contact pressure is highest.
- Duplex or nitrided stainless grades: Duplex 2205 stainless bolts have roughly twice the yield strength and significantly higher hardness than A4, reducing the plastic deformation at thread contact points that initiates galling. For high-torque connections in corrosive environments, duplex grade bolts paired with A4 nuts represent the best balance of galling resistance and corrosion performance.
Self-Tapping Carbon Steel Screws: Thread Form Differences and Their Effect on Pull-Out Strength
Self-tapping screws in carbon steel are not a single product category — the thread form varies significantly between types, and choosing the wrong form for the substrate can result in pull-out forces 30–50% lower than the material would otherwise allow. The ISO 1478 and DIN 7970 type families each optimize thread geometry for a different substrate hardness range, and the difference in flank angle, thread height, and pitch directly determines how much material the screw displaces versus cuts, and how well the formed thread grips under tensile load.
- Type A (coarse pitch, sharp point): Designed for thin sheet metal (0.5–1.5 mm), soft metals, and resin-impregnated plywood. The wide pitch minimizes thread stripping in thin material by maximizing the distance between engaged threads. Not suitable for steel thicker than approximately 1.5 mm — the pitch is too coarse to generate adequate thread engagement depth.
- Type B (fine pitch, blunt point): Suitable for heavier sheet metal (1.5–4.8 mm), die castings, and plastics. The finer pitch creates more thread turns in engagement, increasing pull-out resistance in thicker substrates. The blunt point reduces the risk of piercing adjacent components during assembly in blind-hole applications.
- Type C (machine screw thread, self-tapping): Carries a standard machine screw thread profile (60° flank angle) but is hardened to cut its own thread in pre-drilled holes. Generates significantly higher pull-out strength than Type A or B in steel substrates because the thread profile matches standard nut geometry, maximizing thread flank contact area.
- Thread-rolling (Taptite) type: Forms the thread by displacing material rather than cutting it, producing a work-hardened thread in the substrate that resists loosening under vibration better than cut threads. Preferred in automotive body and structural applications where loosening resistance under dynamic load is critical and re-use of the fastener is not required.
Pilot hole diameter is equally critical: an oversized hole reduces thread engagement and pull-out strength proportionally, while an undersized hole increases driving torque beyond the screw's torsional capacity, causing head shear or torsional fracture before full seating. Substrate material, sheet thickness, and thread type each define a specific pilot hole diameter range — a specification that should be confirmed from the screw manufacturer's technical data, not estimated. Shanghai Soverchannel Industrial Co., Ltd. provides pilot hole recommendations as part of its technical documentation for self-tapping carbon steel screw orders, particularly for customers in the automotive and industrial assembly sectors.
Choosing Between Stainless Steel Bolts and Hot-Dip Galvanized Carbon Steel for Outdoor Structural Connections
When outdoor structural connections require corrosion protection over a 25–50 year design life — curtain wall fixings, bridge inspection walkway hangers, rooftop equipment frames — the choice between Stainless Steel Bolts and hot-dip galvanized carbon steel bolts involves more than a simple cost comparison. Each system has failure mechanisms, maintenance demands, and compatibility constraints that affect total lifecycle cost differently depending on the exposure category and the structural material being joined.
| Factor |
A4-70 Stainless Steel Bolts |
HDG Carbon Steel Bolts (Grade 8.8) |
| Corrosion mechanism |
Pitting in high-chloride environments |
Zinc depletion, then base steel corrosion |
| Expected service life (C3 atmosphere) |
50+ years with no maintenance |
25–35 years before recoating required |
| Galvanic compatibility with aluminum |
Risk — stainless accelerates aluminum corrosion |
Better — zinc potential closer to aluminum |
| Thread fit after coating |
Unchanged — no coating on thread |
Oversize nuts required (6AZ per ISO 10684) |
| Upfront cost (relative, M16) |
3–5× HDG carbon steel |
Baseline |
| Re-tightening after installation |
Galling risk if dry — lubrication required |
Normal — coating provides lubricity |
Galvanic corrosion between stainless steel bolts and aluminum structural members is a frequently underestimated design risk in curtain wall and cladding systems. In the galvanic series, stainless steel sits far from aluminum in electrochemical potential, making aluminum the sacrificial anode in any wet contact scenario. Where stainless bolts must connect aluminum framing, EPDM isolation washers and nylon sleeves that physically separate the metals are the standard mitigation, but this adds to assembly complexity and is often omitted on site. Hot-dip galvanized carbon steel bolts, with zinc potential closer to aluminum, are galvanically compatible without isolation hardware and represent the simpler and safer choice for aluminum-framed structures in non-marine environments.
Shanghai Soverchannel Industrial Co., Ltd. supplies both stainless steel and carbon steel bolt systems with matched coating and material documentation, giving structural engineers and procurement teams the data needed to make the correct selection for their specific exposure category and substrate combination — rather than defaulting to one material across all applications.