Industry Knowledge
How Flange Tooth Geometry Generates Anti-Loosening Force Without Secondary Components
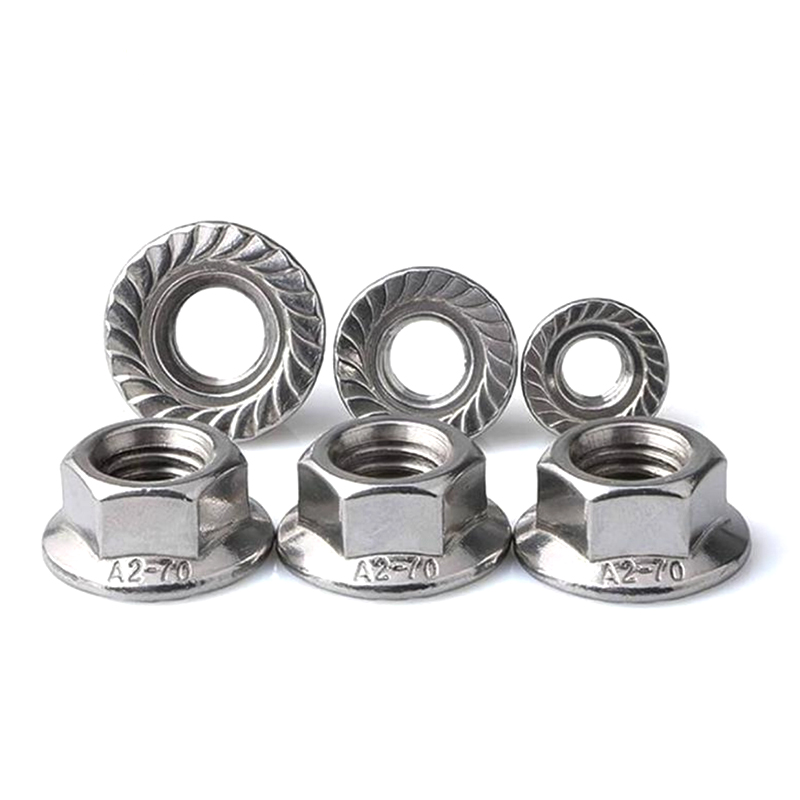
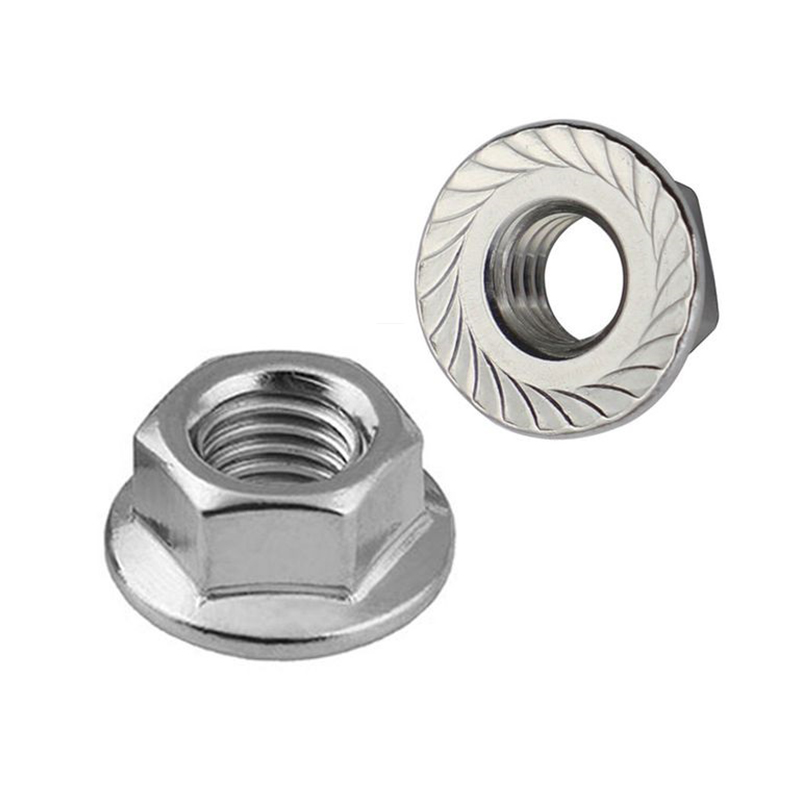
The anti-loosening mechanism of a Hex Flange Nut Non-Slip Nuts design is fundamentally different from prevailing-torque methods such as nylon inserts or deformed thread locking nuts. Rather than increasing the resistance to rotation within the thread interface, the serrated flange operates at the bearing face — the contact surface between the nut and the substrate — by converting the axial clamp load into a mechanical interlock that resists rotation directly at the joint face. This distinction matters because bearing-face loosening (rotation driven by transverse vibration-induced slip between the nut face and substrate) is the dominant loosening mechanism in high-vibration assemblies, not thread-interface loosening, which is a secondary effect.
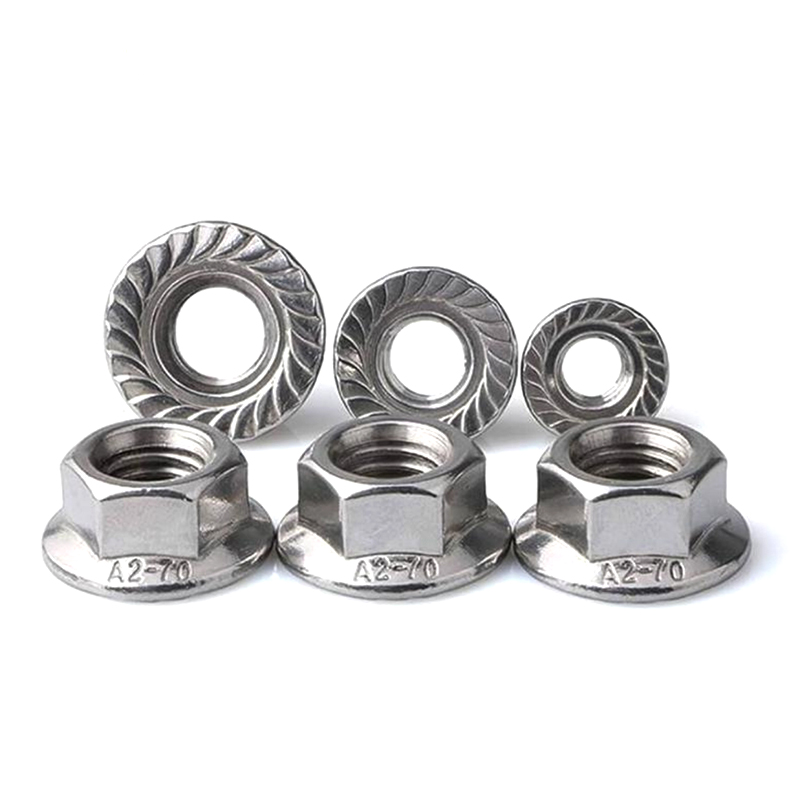
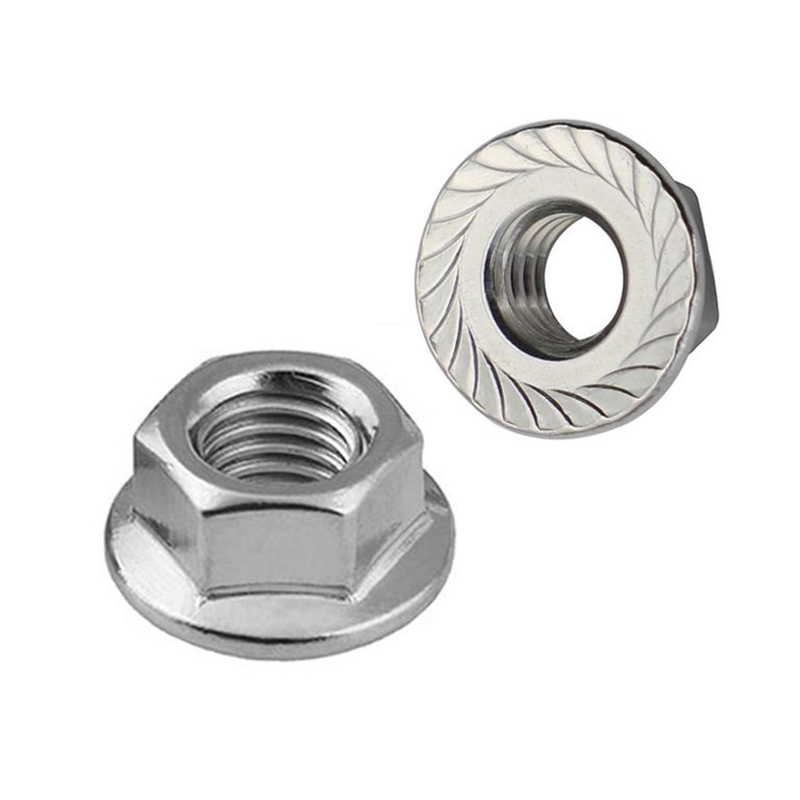
The serrations on the flange face are engineered with a specific asymmetric tooth profile: the leading edge (in the tightening direction) has a shallow ramp angle of approximately 15–20°, while the trailing edge (in the loosening direction) is nearly radial, with a face angle of 75–90°. This asymmetry is the key to the non-slip function. During tightening, the shallow ramp allows the tooth to ride up over the substrate surface without generating excessive installation torque. During any reverse rotation induced by vibration, the near-radial trailing face engages the substrate asperities almost perpendicular to the motion, creating a locking resistance that increases proportionally with the clamp load pressing the flange against the substrate. In practical terms, this means the higher the bolt preload, the more effective the anti-loosening engagement — the opposite behavior from friction-based methods, which degrade as preload is lost through embedding or relaxation.
Tooth depth and tooth count per unit circumference are the two variables that determine bearing-face locking torque for a given clamp load. DIN 6923 serrated flange nuts use a tooth depth of approximately 0.2–0.4 mm depending on nominal diameter, and tooth count is typically 30–60 teeth around the flange perimeter. This geometry produces a locking torque coefficient — the ratio of resisted loosening torque to applied clamp load — of approximately 0.08–0.15, sufficient to prevent loosening under Junker vibration test conditions (DIN 65151) that cause standard hex nuts to fully release within 30 seconds of vibration initiation.
Strength Grade 8.8 vs. 10.9 in Flange Nut Applications: Load Capacity, Hardness, and Substrate Interaction
The choice between Grade 8.8 and Grade 10.9 for Hex Flange Nut Non-Slip Nuts in high-vibration assemblies involves considerations beyond simple load capacity. Because the serrated flange relies on tooth penetration into the substrate surface to generate its locking mechanism, the hardness relationship between the nut flange and the mating surface is as important as the tensile and proof load values used in joint design calculations. A flange nut that is too soft relative to the substrate will have its teeth deformed by the substrate rather than penetrating it — producing a smooth, flat contact area with no mechanical interlocking. A nut that is excessively hard relative to a soft substrate will gouge rather than engage it, generating metal debris and creating stress concentrations that initiate fatigue cracks in the substrate material around the fastener hole.
| Property |
Grade 8.8 Flange Nut |
Grade 10.9 Flange Nut |
| Proof Load (MPa) |
600 |
830 |
| Hardness Range (HRC) |
22–32 |
32–39 |
| Paired Bolt Grade |
8.8 |
10.9 |
| Suitable Substrate Hardness |
HRB 70–100 (mild to medium steel, aluminum alloy) |
HRB 90–HRC 30 (structural steel, alloy steel castings) |
| Typical Application |
Motor housings, light steel structures, general machinery |
Automotive suspension, construction machinery frames, heavy steel structures |
| Hydrogen Embrittlement Risk |
Low |
Elevated — baking required after electroplating per ISO 4042 |
Mechanical and application comparison between Grade 8.8 and Grade 10.9 DIN 6923 serrated hex flange nuts.
Grade 10.9 flange nuts in automotive and construction machinery applications carry an additional process requirement that is frequently overlooked in procurement: when electroplated, they must undergo hydrogen embrittlement relief baking at 190–210°C for a minimum of 4 hours within 4 hours of plating, as specified in ISO 4042. At HRC 32–39, the carbon steel matrix is susceptible to hydrogen absorption during the acid pickling and electroplating process, which can cause delayed brittle fracture under sustained tensile load — sometimes hours or days after installation. For high-vibration applications where fatigue life is the governing failure criterion, specifying Dacromet or mechanical zinc plating for Grade 10.9 flange nuts eliminates this risk entirely, since neither process involves acid exposure or electrolytic hydrogen generation.
Substrate Surface Condition and Its Effect on Serrated Flange Engagement in Service
The long-term anti-loosening performance of Non-Slip Nuts with serrated flanges is more sensitive to substrate surface condition than most installation specifications acknowledge. The serration engagement depth — typically 0.2–0.4 mm — means that surface coatings, mill scale, paint layers, and corrosion products between the flange and the substrate can fundamentally alter the locking mechanism. When the flange teeth engage through a compressible or friable intermediate layer rather than directly into the base metal, the initial installation appears correct but the locking geometry is supported by the coating rather than the substrate. As the coating creeps or degrades under vibration and thermal cycling, the tooth engagement is progressively lost without any visible change at the nut head.
- Paint and primer layers — Organic coatings above approximately 80–100 µm total thickness (a common range for structural steel primers plus topcoat) will not allow serration teeth to reach the base metal during installation at standard torque values. For painted steel structure connections using Hex Flange Nut Non-Slip Nuts, the fastener zone should be masked during painting, or a spot-face operation performed to expose bare metal in the washer contact area before installation. This is standard practice in automotive body-in-white assembly where painted panels are fastened with serrated flange nuts, but it is frequently omitted in site-installed steel structure applications where surface preparation is less controlled.
- Hot-dip galvanized surfaces — The zinc-iron alloy layer of hot-dip galvanizing (typically 45–85 µm, hardness approximately HV 150–250) is significantly softer than the serrated flange steel. Tooth penetration into galvanized substrate is deeper and more complete than into bare structural steel, which is beneficial for initial engagement. However, the zinc layer's lower fatigue resistance means that repeated vibration loading can cause the tooth impressions in the zinc to progressively widen through micro-plastic deformation, gradually reducing the mechanical interlock. In galvanized steel structure connections subject to long-term dynamic loading, periodic torque verification at 12-month intervals is recommended as part of the maintenance schedule.
- Aluminum alloy substrates — Motor housings and construction machinery castings in aluminum alloy (typically 6061-T6 or A380 die-cast) present a substrate hardness of HRB 60–75 — at the lower boundary of the Grade 8.8 flange nut's effective engagement range. For aluminum substrates, reducing the tooth pitch (increasing tooth count) and using a larger flange diameter distributes the engagement load over more teeth and prevents localized yielding of the substrate that would allow the nut to embed fully and lose its anti-loosening function over time. Some applications additionally specify a hardened steel insert plate or captive washer between the serrated flange and the aluminum surface to provide a compatible hardness interface without sacrificing the locking mechanism.
As a manufacturer with deep experience supplying precision fasteners to the automotive industry — where serrated flange nuts are used in high-cycle vibration environments and surface condition control is integral to the production process — Shanghai Soverchannel Industrial Co., Ltd. provides application engineering guidance on substrate compatibility as part of its customer support, ensuring that the specified Hex Flange Nut Non-Slip Nuts perform as designed throughout the service life of the assembly.
Reusability Limits and Inspection Criteria for Serrated Flange Nuts in High-Reliability Applications
Serrated flange nuts are more reuse-limited than standard hex nuts, yet maintenance and repair procedures in construction machinery and motor servicing frequently treat them as freely reusable components. Understanding the mechanics of tooth wear and the inspection criteria that define the reuse boundary is essential for maintaining joint reliability in applications where loosening failure has significant safety or operational consequences.
Each installation cycle plastically deforms the tooth tips as they embed into the substrate and causes micro-abrasion on the tooth flanks during the tightening rotation. After the first installation, the tooth geometry is partially altered: the near-radial trailing faces that provide loosening resistance are slightly rounded by the embedding process, and the substrate impressions from the first installation remain as shallow recesses. On reinstallation in the same location, the teeth re-engage the existing impressions with less plastic deformation, resulting in reduced effective tooth engagement depth and lower locking torque coefficient compared to first installation. Research on DIN 6923 serrated flange nuts in automotive applications indicates that the locking torque coefficient degrades by approximately 15–25% between first and second installation, and by a further 10–15% on each subsequent cycle.
- Visual inspection criteria for reuse — Tooth tips should show no visible rounding or flattening when viewed under 10× magnification. The flange bearing face should be free of radial scoring marks wider than 0.1 mm, which indicate excessive slip during previous installation. Any evidence of flange deformation — visible distortion of the flat-to-flat geometry or non-perpendicularity of the flange face to the thread axis — is grounds for rejection regardless of service cycle count.
- Maximum reuse cycles by application criticality — For automotive safety-critical connections (suspension, steering, braking systems), DIN 6923 flange nuts are typically specified as single-use components and must be replaced at every disassembly. For general construction machinery and motor mounting applications, two installation cycles are the practical limit before locking performance degrades below the threshold for vibration-prone service. Steel structure connections that are only torqued once and never intentionally loosened are not subject to reuse cycle limits but should be inspected for corrosion-induced tooth degradation during scheduled maintenance intervals.
- Substrate reuse considerations — Even when a new flange nut is installed, previously tooth-marked substrate surfaces provide less resistance to the new nut's teeth than virgin material. In critical applications requiring guaranteed locking performance on reassembly, the substrate surface in the fastener zone should be restored by machining or grinding to expose a fresh bearing face, or a hardened washer should be interposed to provide a new engagement surface without modifying the structural member.
With a full-process inspection system developed through years of precision fastener manufacturing for the automotive sector, Shanghai Soverchannel Industrial Co., Ltd. produces Hex Flange Nut Non-Slip Nuts to DIN 6923 dimensional and mechanical requirements with documented tooth geometry verification, providing customers in automobile, construction machinery, motor, and steel structure applications with the quality traceability needed for high-reliability locking performance from first installation through the specified service life.